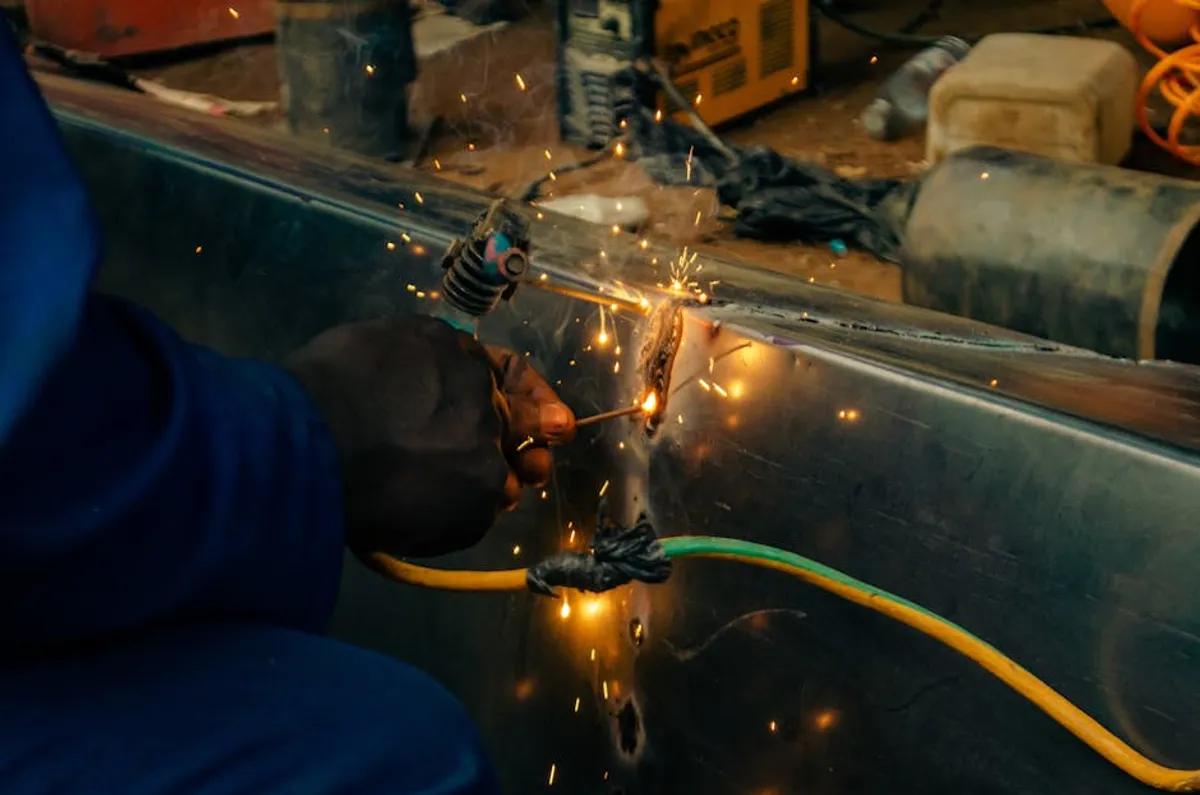
Achieving consistent, high-quality MIG welds hinges significantly on precise gas pressure management. The shielding gas protects the molten weld pool from atmospheric contaminants like oxygen and nitrogen, which would otherwise cause defects such as porosity and embrittlement. Incorrect gas pressure, whether too high or too low, directly impacts this protective envelope, leading to compromised weld integrity, increased rework, and wasted consumables. Understanding the specific requirements for different gases, materials, and welding conditions is not merely a technical detail; it is a critical operational factor influencing production efficiency and the structural soundness of your finished products.
Fundamentals of MIG Welding Shielding Gas Pressure
MIG welding relies on an inert or semi-inert gas shield to prevent oxidation and contamination of the weld pool. The pressure at which this gas is delivered directly influences its effectiveness. It's not about maximizing pressure, but about optimizing the flow rate to create a stable, consistent shield around the arc and molten metal. Too little pressure allows ambient air to infiltrate, causing porosity and poor fusion. Too much pressure can create turbulence, drawing in atmospheric contaminants, cooling the weld pool too rapidly, or even wasting gas unnecessarily.
Common Shielding Gas Types and Their Pressure Needs
The choice of shielding gas dictates the appropriate pressure range, as different gases have varying densities and flow characteristics. Regulators and flowmeters are calibrated to provide accurate readings for specific gas types.
- Argon (Ar): Often used for aluminum and non-ferrous metals. Argon provides a stable arc and good penetration. Typical flow rates range from 15-25 cubic feet per hour (CFH) for light to medium fabrication.
- Carbon Dioxide (CO2): A reactive gas primarily used for steel, offering good penetration and cost-effectiveness. However, it can produce more spatter and a harsher arc than argon mixes. Flow rates are often similar to argon, around 15-25 CFH, adjusted based on material thickness and wire diameter.
- Argon/CO2 Mixes: The most common choice for steel welding, balancing the benefits of both gases. For instance, 75% Argon / 25% CO2 (C25) is popular for short-circuit MIG, providing a stable arc, reduced spatter, and good bead appearance. Flow rates typically fall within the 20-30 CFH range, depending on the specific mix and application.
- Argon/Oxygen (Ar/O2) Mixes: Small additions of oxygen (1-5%) to argon improve arc stability, wetting action, and bead profile for spray transfer on stainless steel and some carbon steels. Flow rates are generally in the 25-35 CFH range.
Key Factors Influencing Gas Pressure Settings
Optimal gas pressure is not a static value; it requires adjustment based on several variables to maintain weld quality and efficiency.
Material Thickness: Thicker materials often require higher amperage and wire feed speed, which in turn necessitates a slightly higher gas flow rate to adequately shield the larger weld pool and longer arc time. A thin sheet metal weld might use 15 CFH, while heavy plate could demand 30 CFH or more.
Wire Diameter: Larger diameter welding wires typically run at higher amperages, producing a larger, hotter weld pool. This increased energy input requires a more robust gas shield, often achieved with a slightly elevated flow rate.
Welding Position: Out-of-position welding (vertical, overhead) can sometimes benefit from slightly increased gas flow to ensure the shielding gas effectively covers the molten puddle against gravity and convection currents.
Joint Type and Geometry: Deep grooves or complex joint designs might require specific nozzle angles or slightly higher flow rates to ensure complete gas coverage into confined spaces.
Environmental Conditions: Drafts from open doors, fans, or air conditioning systems can disrupt the shielding gas envelope, leading to porosity. In such cases, increasing the gas flow rate or erecting physical barriers (wind screens) becomes necessary. However, excessively high flow rates to combat drafts can also cause turbulence and draw in contaminants.
Pro Tip: Always check for gas leaks before starting any welding operation. Even small leaks in hoses, fittings, or the torch can significantly reduce the effective shielding gas flow, leading to porosity and inconsistent welds, even if your flowmeter indicates a correct setting. Use a leak detection solution (soapy water) on all connections.
Setting and Adjusting Gas Pressure for Optimal Welds
Accurate gas pressure management involves understanding the function of your equipment and knowing how to interpret visual cues from the weld.
Regulator and Flowmeter Function
A gas regulator reduces the high pressure from the gas cylinder to a usable working pressure. The flowmeter then measures and controls the volume of gas flowing through the torch per unit of time (typically in CFH or liters per minute, LPM). For MIG welding, a flowmeter is essential because it directly indicates the volume of gas delivered, which is the critical parameter for shielding, rather than just the pressure within the line.
Troubleshooting Common Gas-Related Weld Issues
Incorrect gas pressure or flow can manifest in several weld defects:
- Porosity: Small holes or voids in the weld bead, often caused by insufficient gas shielding allowing atmospheric gases into the molten pool. This indicates flow is too low, or there are drafts/leaks.
- Excessive Spatter: While not solely gas-related, too high a CO2 content in the mix or excessive gas flow creating turbulence can contribute to spatter, leading to more post-weld cleanup.
- Poor Penetration/Fusion: While primarily related to amperage and wire feed, an unstable arc due to inadequate shielding can indirectly affect penetration.
- Sooting/Black Deposits: Can indicate an issue with gas type, flow, or contamination. For aluminum, black soot often points to insufficient cleaning or improper gas selection.
Adjusting the flowmeter in small increments (2-5 CFH) and observing the weld bead is the most effective method for fine-tuning. A consistent, smooth arc and a clean, uniform bead without excessive spatter or porosity are indicators of correct gas flow.
Essential Equipment for Gas Pressure Management
Reliable equipment is fundamental for consistent gas delivery and weld quality.
Gas Regulators: These devices attach to the gas cylinder and reduce the high cylinder pressure to a manageable working pressure. Look for regulators with clear, easy-to-read gauges for both cylinder pressure and outlet pressure. Single-stage regulators are common for MIG, while two-stage regulators offer more consistent outlet pressure as the cylinder empties, beneficial for critical applications.
Flowmeters: Crucial for MIG welding, flowmeters measure the actual gas flow rate in CFH or LPM. Ball-type flowmeters (with a floating ball in a tapered tube) are common and provide a visual indication of flow. Some regulators integrate a flowmeter directly. Ensure the flowmeter is calibrated for the specific gas you are using, as gas density affects readings.
Hoses and Fittings: High-quality, gas-specific hoses and secure fittings are necessary to prevent leaks and ensure consistent gas delivery from the cylinder to the welding torch. Use proper clamps and inspect hoses regularly for cracks or wear.
Buying Considerations for Regulators and Flowmeters
When selecting gas management equipment, prioritize features that contribute to accuracy, durability, and compatibility with your welding setup.
Gas Type Compatibility: Ensure the regulator and flowmeter are designed for the specific shielding gas you will be using (e.g., Argon, CO2, Argon/CO2 mixes). Different gases have different connection threads and calibration requirements.
Gauge Clarity and Durability: Opt for regulators with large, easy-to-read gauges protected by a robust casing to withstand workshop environments. Stainless steel components offer enhanced corrosion resistance.
Flow Rate Range: Select a flowmeter with a range that comfortably covers your typical welding applications. A range of 0-60 CFH is common for general MIG work.
Connection Type: Verify that the regulator's inlet connection matches your gas cylinder's valve. Common connections include CGA 580 for inert gases (Argon, Helium) and CGA 320 for CO2.
Material Construction: Brass body construction is standard for regulators, offering durability and resistance to gas corrosion. Internal components should also be robust for longevity.
Optimizing Your MIG Welds Through Gas Pressure
Effective management of MIG welding gas pressure is a foundational element for producing high-quality, defect-free welds. It directly impacts arc stability, bead appearance, and the mechanical properties of the weld metal. By consistently monitoring flow rates, adjusting for environmental factors, and understanding the specific needs of different shielding gases, welders can significantly reduce costly rework, minimize material waste, and enhance overall productivity. Regular equipment maintenance, including leak checks and flowmeter calibration, ensures that the protective gas shield remains effective throughout the welding process, contributing to both operational efficiency and the integrity of the final product.
Frequently Asked Questions About MIG Welding Gas Pressure
Q: What is the ideal gas pressure for MIG welding steel with C25 gas?
A: For most steel applications using 75% Argon / 25% CO2 (C25), a flow rate of 20-30 CFH (cubic feet per hour) is a good starting point. Adjust based on material thickness, wire diameter, and environmental conditions.
Q: Can too much gas pressure be detrimental?
A: Yes, excessive gas pressure can create turbulence around the weld pool, drawing in atmospheric contaminants and leading to porosity. It also cools the weld pool too quickly and wastes shielding gas.
Q: How do I check for gas leaks in my MIG setup?
A: Apply a soapy water solution to all gas connections (regulator, hoses, torch connections) with the gas supply open. Bubbles indicate a leak. Ensure all fittings are tight and hoses are in good condition.
Q: Is there a difference between gas pressure and gas flow rate?
A: Yes. Gas pressure refers to the force exerted by the gas within the lines, typically measured in PSI. Gas flow rate, measured in CFH or LPM, is the volume of gas delivered to the weld area per unit of time. For MIG welding, the flow rate is the critical parameter for effective shielding.
Start the conversation
Thoughtful disagreement welcomed. Promotional links quietly removed.